PETG vs ABS comes down to one trade-off: PETG is stronger and much easier to print, while ABS is tougher, handles more heat, and can be smoothed with acetone. This guide compares the two with datasheet numbers and shows which one to pick for your part.
All figures below come from Polymaker’s PolyLite PETG and PolyLite ABS datasheets. Both were printed and tested the same way, as solid 100% infill bars, so the comparison is fair. Other brands will differ by a few percent, but the pattern holds.
The Short Answer
- Choose PETG for brackets, enclosures, and functional parts that stay below about 70 °C. It is roughly 50% stronger in tension, needs no enclosure, and barely smells.
- Choose ABS for parts that take knocks, sit near heat between 70 and 95 °C, or need a smooth acetone finish. Print it in an enclosure with ventilation.
- Neither is the best choice for long-term sunlight. For outdoor parts, look at ASA, ABS’s UV-resistant cousin.
PETG vs ABS Comparison Table
| Property | PETG | ABS |
|---|---|---|
| Tensile strength, along layers | 50.8 MPa | 33.4 MPa |
| Tensile strength, across layers | 42.8 MPa | 29.7 MPa |
| Flexural strength | 69.6 MPa | 56.2 MPa |
| Tensile modulus (stiffness) | 2,117 MPa | 2,247 MPa |
| Elongation at break, along layers | 8.4% | 17.9% |
| Notched impact strength (Charpy) | 2.6 kJ/m² | 18.0 kJ/m² |
| Heat deflection temperature, 1.8 MPa | 75 °C | 98 °C |
| Glass transition | 81 °C | 101 °C |
| Density | 1.25 g/cm³ | 1.04 g/cm³ |
| Water absorption at equilibrium | 0.54% | 0.35% |
| Nozzle temperature | 230–260 °C | 245–265 °C |
| Bed temperature | 70–80 °C | 90–100 °C |
| Enclosure | Not needed | Needed |
| Acetone smoothing | No | Yes |
Strength: PETG Wins in Tension and Bending
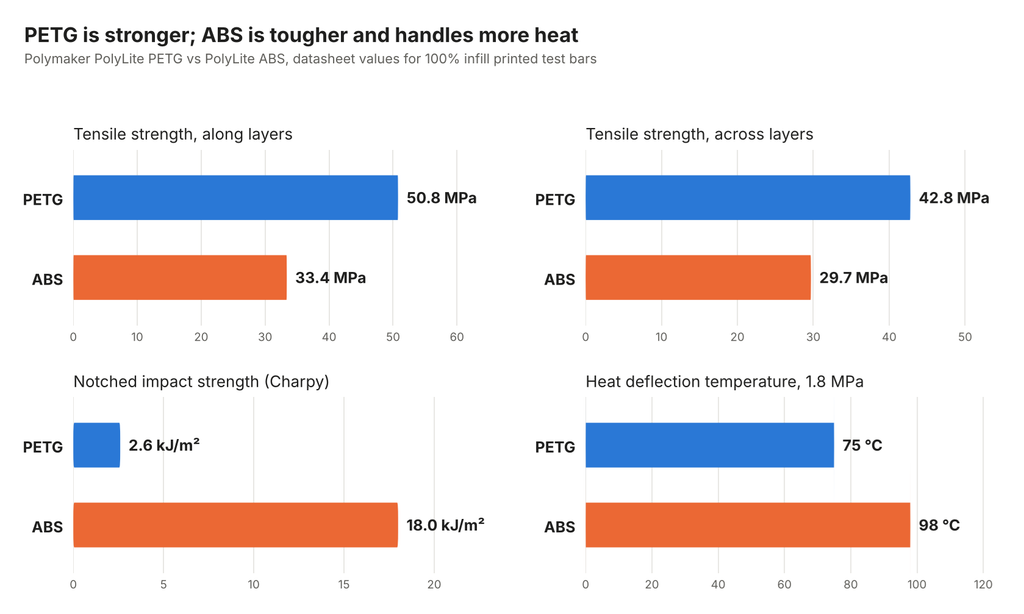
PETG is the stronger material. Along the layers it reaches 50.8 MPa against 33.4 MPa for ABS, about 52% more. Across the layers, where printed parts usually fail, the gap is similar: 42.8 MPa against 29.7 MPa.
PETG also bonds its layers well. It keeps about 84% of its strength across the layers, close to ABS’s 89%, and both are far better than a part that delaminates. In bending, PETG leads 69.6 MPa to 56.2 MPa.
Stiffness is close. ABS is slightly stiffer, by about 6% in tension and 12% in bending, which rarely decides a design on its own.
Remember that these are solid test bars. A real part with 20% infill and two walls will carry far less, whichever material you use. Walls and orientation matter more than the filament choice; see our guide to the best infill for strength.
Toughness and Impact Strength: ABS Wins Clearly
Toughness is where ABS earns its place. In a notched Charpy test, ABS absorbs 18.0 kJ/m², about seven times PETG’s 2.6 kJ/m². ABS also stretches more before it breaks: 17.9% against 8.4%.
The notch matters. A notched test shows how a material behaves at a sharp corner, a crack, or a layer line, which is where printed parts break. PETG flexes nicely in a smooth part, but a sharp internal corner can let a crack run through it. ABS tolerates those stress raisers much better.
In practice:
- Parts that get dropped, hit, or snapped together repeatedly favor ABS.
- Parts that carry a steady load without shocks favor PETG.
- With either material, add fillets to inside corners. It costs nothing and removes the notch that starts most cracks.
Heat Resistance: ABS Takes About 23 °C More
The heat deflection temperature is the temperature at which a loaded test bar starts to bend. At 1.8 MPa, ABS reaches 98 °C and PETG 75 °C. The glass transition, where the plastic starts to soften, follows the same pattern: 101 °C for ABS, 81 °C for PETG.
Use those numbers with a margin. A part that carries load should stay well below its heat deflection temperature.
| Where the part lives | PETG | ABS |
|---|---|---|
| Indoors, room temperature | Yes | Yes |
| Electronics enclosure, warm but below 60 °C | Yes | Yes |
| Car interior in summer, can exceed 70 °C | Risky | Yes |
| Near a motor, heater, or hot end, 80–95 °C | No | Borderline; test it |
Printing PETG and ABS
PETG is the easier filament. It prints at 230–260 °C on a 70–80 °C bed, needs no enclosure, and warps very little. Its main habits are stringing and sticking too well: on a smooth PEI sheet it can pull chunks out of the surface, so use a textured sheet or a thin layer of glue stick as a release.
ABS is harder work. It needs 245–265 °C, a 90–100 °C bed, the part cooling fan off, and an enclosure. ABS shrinks as it cools, so without a warm chamber, large parts lift at the corners and tall parts crack between layers.
| Setting | PETG | ABS |
|---|---|---|
| Nozzle | 230–260 °C | 245–265 °C |
| Bed | 70–80 °C | 90–100 °C |
| Part cooling fan | Off to 20% | Off |
| Enclosure | Not needed | Needed |
| Main problem | Stringing, sticking to smooth PEI | Warping and layer cracking |
| Drying before use | 65 °C for 6 hours | 70 °C for 6 hours |
Fumes and Ventilation
ABS has a strong smell while printing, and it releases more fine particles than most filaments. In one published office test, an ABS printer emitted about ten times more ultrafine particles per minute than a PLA printer. Print ABS in a room with good ventilation or in an enclosure with a filter.
PETG has only a mild smell. Every filament releases some particles when melted, so ventilation is still a good idea, but PETG is the easier choice for a shared office or a classroom.
Moisture, Chemicals, and Outdoor Use
PETG absorbs more water from the air than ABS, 0.54% against 0.35% at equilibrium. Wet PETG strings, pops, and prints weaker parts, so dry it before printing and store it sealed.
The two resist different chemicals. Acetone dissolves ABS, which is a problem near solvents and an advantage for smoothing. PETG is not affected by acetone in the same way, and it handles water well.
Outdoors, PETG holds up better than ABS. ABS yellows and becomes brittle in sunlight within months. For parts that live outside for years, ASA is the better option; we compare it in ASA vs ABS.
Post-Processing and Acetone Smoothing
Acetone smoothing is a major reason to choose ABS. A short exposure to acetone vapor melts the outer surface, hides the layer lines, and gives a glossy finish. It also seals the surface and slightly improves layer bonding at the skin.
PETG cannot be smoothed this way. To finish PETG, sand it, use a filler primer, and paint. ABS also sands and glues easily; acetone works as a solvent glue for joining ABS parts.
Weight and Cost per Part
PETG is denser: 1.25 g/cm³ against 1.04 g/cm³ for ABS. The same part printed in PETG weighs about 20% more, and a 1 kg spool of PETG prints about 20% less volume. When both cost the same per kilogram, ABS is the cheaper material per part.
Which Should You Choose?
The ABS vs PETG decision depends on what the part has to survive:
| Part | Better choice | Why |
|---|---|---|
| Brackets, mounts, jigs | PETG | Higher strength, easy to print |
| Electronics enclosures | PETG | Strong, low warp, no fumes in the office |
| Snap-fit clips and parts that get dropped | ABS | Much higher impact strength |
| Car interior parts | ABS | Copes with summer cabin heat above 70 °C |
| Parts near motors or heaters | ABS | About 23 °C higher heat deflection temperature |
| Display parts with a glossy finish | ABS | Acetone smoothing |
| Water-contact parts and containers | PETG | Handles water well |
| Long-term outdoor parts | ASA | Neither PETG nor ABS resists UV for years |
For a wider comparison that includes PLA, see PLA vs ABS vs PETG.
PETG vs ABS FAQ
Is ABS stronger than PETG?
No, not in tension or bending. PETG is about 50% stronger in tension along the layers. ABS is tougher, though: it absorbs about seven times more energy in a notched impact test, so it survives knocks and drops better.
Is PETG more heat resistant than ABS?
No. ABS has a heat deflection temperature of about 98 °C at 1.8 MPa, while PETG reaches about 75 °C. For parts above 70 °C, such as car interior parts, choose ABS.
Can PETG be smoothed with acetone?
No. Acetone smoothing works on ABS and ASA, not on PETG. PETG parts are finished by sanding, priming, and painting.
Do I need an enclosure to print PETG?
No. PETG prints well in an open printer. ABS needs an enclosure to stop warping and layer cracking, especially on larger parts.
Is PETG or ABS better for outdoor use?
PETG holds up better than ABS, which yellows and turns brittle in sunlight. For parts that stay outdoors for years, ASA is the better choice than either.
Need a Part That Has to Survive Heat or Impact?
RunTechEngineer chooses the material from what the part has to do: the load, the temperature, and the environment it will live in. Explore our 3D printing services or Contact Us to discuss your part.